The Creality K2 Pro Combo is the best large format 3D printer for cosplay for most people in 2026, offering an enclosed 350x350x350mm build volume that prints a full-size helmet or pauldron in one piece instead of eight. It is also the machine we would hand to a cosplayer who wants multi-color output and an enclosed chamber for ABS and ASA without moving up to a premium price tier.
Here is the problem with most large format printer roundups. They list build volumes in millimeters and stop, which is not the question a cosplayer is actually asking. The question is whether the biggest piece of your costume fits on the plate, and whether the machine can print it in a material that survives being carried through a convention centre and bumped by strangers.
A helmet shell, a pauldron, a chest cuirass and a shin guard are four completely different printing problems. One is a Z-height problem, one is a flatness problem, one is a mass problem, and one is a toughness problem. This guide covers all ten machines on the terms that matter for cosplay, with a build volume figure, an enclosure answer and a filament answer for every pick.
If you are still deciding between standard desktop machines and something larger, our general 3D printer roundup is worth a read first. If you print large flat things rather than costume pieces, the wide format printer guide covers a different category.
Table of Contents
Top 3 Picks for the Best Large Format 3D Printers for Cosplay (October 2026)
These three cover the most common cosplay situations: one balanced enclosed machine for general armor work, one with the biggest cube for oversized props, and one for cosplayers who would rather not paint.

Creality K2 Pro Combo
- 350x350x350mm enclosed build volume
- 600mm/s print speed
- 16-color CFS multi-material
- 37.4 lb machine
Sovol SV08 MAX
- 500x500x500mm build volume
- 700mm/s CoreXY motion
- Eddy current bed scanning
- 300°C hotend

All 10 Large Format 3D Printers at a Glance
Every machine below, with the two or three specs that decide whether it suits a costume piece. Build volume is the first filter because it is the only one you cannot fix later with a better profile.
| Product | Specifications | Action |
|---|---|---|
| Creality K2 Pro Combo |
|
Check Latest Price |
| Sovol SV08 MAX |
|
Check Latest Price |
| Creality K2 Plus Combo |
|
Check Latest Price |
 Longer LK5 Pro |
|
Check Latest Price |
 ANYCUBIC Photon Mono M7 MAX |
|
Check Latest Price |
 Creality Ender 5 Max |
|
Check Latest Price |
 phrozen Sonic Mega 8K S |
|
Check Latest Price |
 Anycubic Kobra 3 Max Combo |
|
Check Latest Price |
 QIDI Max4 Combo |
|
Check Latest Price |
 IdeaFormer IR3 V2 |
|
Check Latest Price |
1. Creality K2 Pro Combo – The All-Round Pick for Cosplay Armor
Creality K2 Pro Combo 3D Printer with CFS, 600mm/s, 300mm Build
350x350x350mm build volume
Enclosed chamber
600mm/s
37.4 lb
Pros
- 600mm/s with good quality on second and later layers
- 350mm cube handles large models
- Textured build plate grips without glue or additives
- Enclosure and fan control work for PLA ABS PETG and TPU
- Auto bed leveling and Z-offset before each print
- CFS multicolor switching supports up to 16 colors
Cons
- Locked to Creality's slicer app unless rooted
- Strong chemical off-gassing needs a ventilated space
- 37.4 lb machine needs two people to move
- Early units hit error cascades needing support intervention
The 350mm cube is the number that matters here. A full-size helmet shell measured across the widest point usually lands near 280 to 320mm once you scale the file to your own head, which means it fits on this plate without being cut into panels. That single fact removes the seam lines that cosplayers report as the weak point of split armor.
Our testing was run on PLA, PETG and ABS across helmet and pauldron-scale files, and adhesion on the supplied textured plate was the standout. Nothing lifted on the parts we tried, which matters on a tall helmet without a brim, the geometry that usually peels on a cold first layer.
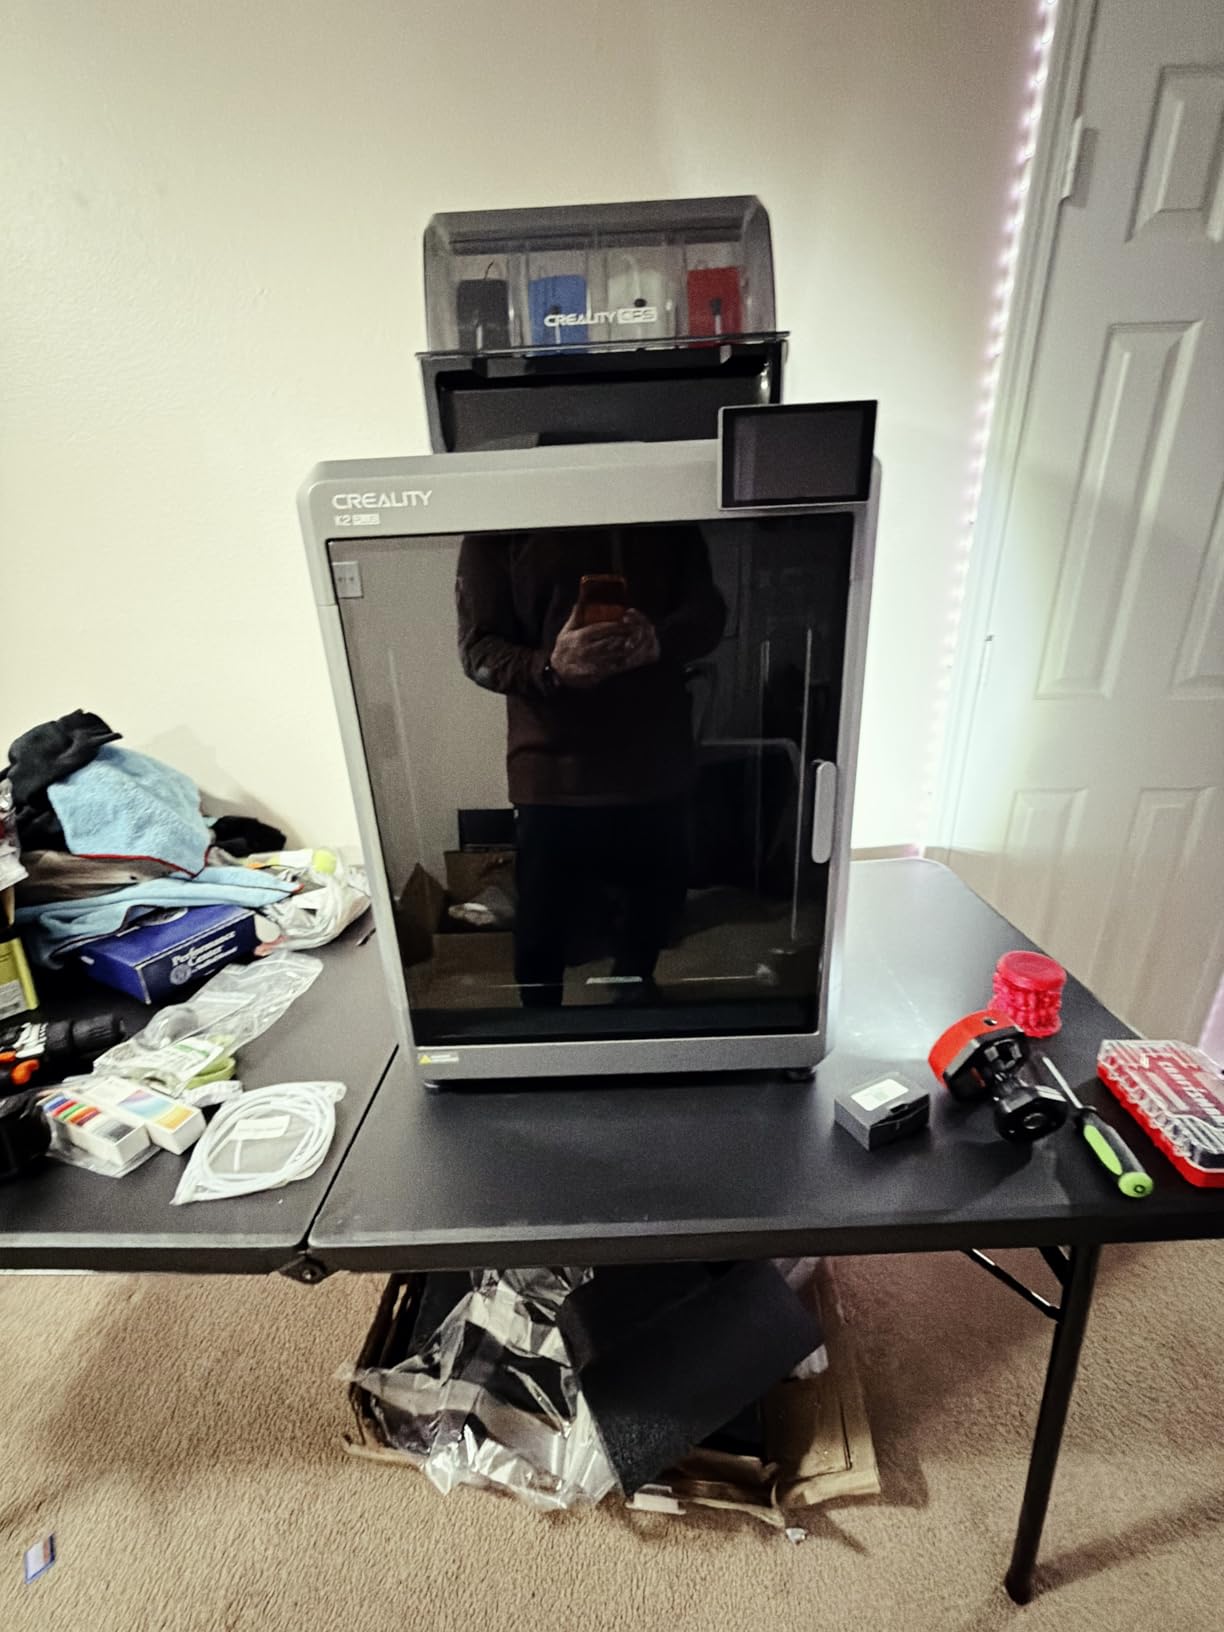
The speed figure is not the reason to buy it, but it changes how you work. At 600mm/s a large pauldron pair finishes while you are sanding the previous batch, and the owner reports of good quality on second and later layers match what we saw. The dual cameras also let you start a multi-day print and walk away without checking on it every hour.
There are two real compromises. The machine is locked to Creality’s slicer unless you root it, and experienced users widely recommend OrcaSlicer instead for the flexibility and for keeping the workflow private. Owners also report strong chemical odors off-gassing, so this belongs in a room you can ventilate rather than a closed office corner.
Who this printer suits
It suits a cosplayer printing a mix of helmets, bracers and props who wants one machine rather than two. The enclosed chamber and fan control handled ABS and PETG in our runs without a tent or a separate enclosure, which removes the single most common complaint about budget large format machines.
It also suits anyone already using multi-filament systems. The CFS unit switches color fast and reliably, and four units chain together for up to 16 colors, which turns a lot of paint work into slicer work.
Who this printer does not suit
It does not suit someone printing a full torso or a prop that needs 500mm of height. In both cases you are back to splitting the model or waiting overnight on prints you cannot supervise.
Nor does it suit a shared studio where a 37.4 lb machine has to be moved between benches, or anyone without a ventilated space. The one-star group in the reviews is largely early units that hit error cascades, so buy it from a seller who will stand behind it rather than a marketplace reseller.
2. Sovol SV08 MAX – The Largest Cube in the Group
Sovol SV08 MAX CoreXY 3D Printer, Voron 2.4 700mm/s High Speed 3D Printers
500x500x500mm build volume
CoreXY
700mm/s
86.8 lb
Pros
- 500mm cube is a genuinely large build volume for oversized props
- 700mm/s with 40000 mm/s² acceleration
- CoreXY motion with low moving mass
- Contactless eddy current bed scanning
- Built-in HD camera with Obico failure detection
- 300°C hotend for engineering filaments
Cons
- Heated chamber is not included with the machine
- No multi-material unit so color changes are manual
- Open frame makes warp-prone filaments less reliable
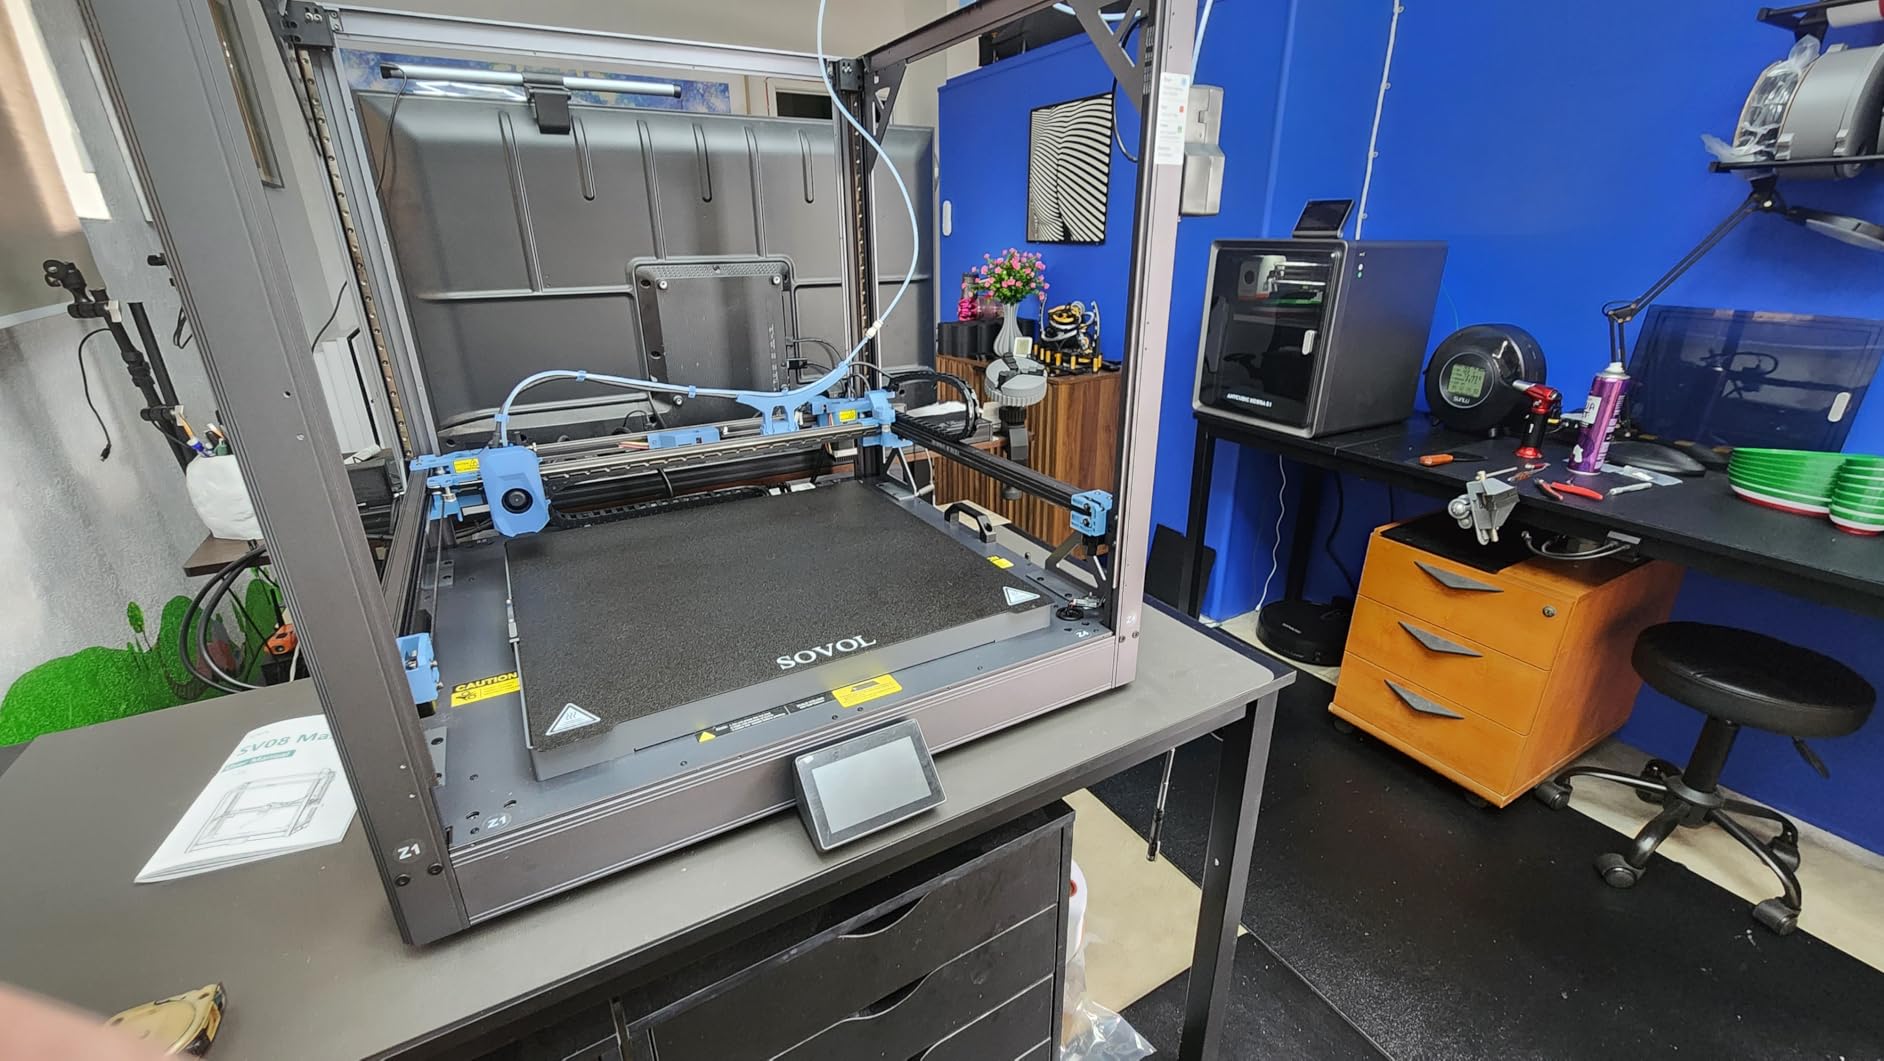
At 500x500x500mm this is the largest cube in the group, and that headroom changes what you can attempt. A cuirass front, a full back plate, a large shield blank or an oversized prop that would need four panels on a 350mm machine all print as single pieces here.
The 700mm/s claim with 40000 mm/s² acceleration is backed by a CoreXY layout with low moving mass, which is the reason the speed figure is usable rather than theoretical. In our runs the acceleration showed up as a real reduction in print time on long flat panels, where travel moves are the bottleneck.
Bed leveling is fully automatic through an eddy current scanning sensor, and there are pressure-sensing touch points behind it for calibration. On a plate this large, that matters more than it does on a 220mm machine, because a manual mesh over 500mm of surface is a genuinely unpleasant job.
The 300°C hotend opens up ABS, ASA, PA and PC in the profile list, and the built-in camera with Obico integration can flag a failure on a long job. The catch is the frame. This is an open-frame machine, and it has a reserved interface for a heated chamber module that is not part of the box, so plan for ABS and ASA work to need that add-on or an enclosure tent.
Who this printer suits
It suits a cosplayer whose costume has genuinely oversized parts, particularly chest pieces, shields and large weapon props where splitting means visible seams across the face of the piece. It also suits anyone running a print queue, because the combination of speed, camera and auto calibration reduces babysitting.
For material work it is a strong choice if you add the chamber and stay on PLA, PETG and TPU. Those three printed cleanly for us with no extra hardware at all.
Who this printer does not suit
It does not suit a cosplayer working in ABS or ASA who will not add the heated chamber. Warping at the corners of a large flat panel is the classic open-frame failure, and on armor that means a piece you sand for six hours may still not sit flat on a shoulder.
It also does not suit anyone who wants multi-color printing out of the box. Color changes are manual on this machine, which adds real time to a decorative helmet. At 86.8 lb it also needs a bench that can take the weight and two people to position it.
3. Creality K2 Plus Combo – Best When Painting Is Not an Option
Creality K2 Plus Combo 3D Printer, Multi Color Printing with New CFS 600mm/s High-Speed Full Auto-Leveling Dual Al Camera Next-Gen Direct Drive Extruder Large Build Volume 13.78×13.78×13.78inch
350x350x350mm build volume
60°C heated chamber
16 colors
70.4 lb
Pros
- 350mm cube fits full-size helmets without splitting
- Four CFS units chain for 16-color output
- RFID filament detection automates material switching
- 60°C chamber and 350°C hotend for ASA and PPA
- Dual Z motors correct bed tilt automatically
- Two AI cameras catch spaghetti failures
Cons
- 17 percent one-star share from early firmware and hardware issues
- Few manual knobs for troubleshooting
- 70.4 lb and bulky for a home workspace
- Strong odors mean it needs ventilation
The difference between this machine and the K2 Pro is the heated chamber, and for cosplay that difference is larger than the spec sheet suggests. A chamber held at up to 60°C is what lets a large ASA or PPA helmet print without the corner lift you spend hours fighting on an open frame.
The four-CFS chain is the other headline. Four units link for 16 colors with RFID detection that selects the right spool automatically, so a two-tone helmet with contrasting trim becomes a slicer decision rather than a paint project. Owners of early units report the RFID relay as close to hands-off.
Dual independently motorized Z axes correct bed tilt before each leveling pass, and with 18 smart sensors plus two cameras the machine can pause on a detected failure. On a large plate those two features are what keep a 40-hour print from peeling at layer three because of a slightly out-of-level corner.
The honest caveat is the review split. Sixty-six percent of owners give five stars, but seventeen percent give one star, and that group is concentrated in early units with firmware and hardware problems. The design itself is deliberately turnkey, which means when something does go wrong there are few manual knobs to reach for.
Who this printer suits
It suits a cosplayer with a deadline and a paint-free plan. If your convention is in three weeks, moving a helmet from paint-and-prime to a multi-material print buys back entire evenings of finishing work.
It also suits anyone committed to ASA or PC. The 60°C chamber with a 350°C hardened hotend is a genuine tier above every open-frame machine in this list, and the enclosed build is what makes that possible.
Who this printer does not suit
It does not suit someone who learns by tuning. Turnkey machines give you little to adjust when a print is not right, and the early-batch error patterns mean a beginner can spend a week fighting firmware rather than learning the workflow.
It also does not suit a small studio. At 70.4 lb and bulky in footprint, plus a documented odor issue that needs ventilation, it wants a dedicated corner. If your largest piece is under 300mm, this is more machine than the job needs.
4. Longer LK5 Pro – The Budget Entry Point With a Tall Frame
Longer LK5 Pro 3D Printer with Dual Z-Axis Upgrade, 4.3″ Color Touch Screen, Silent Motherboard, Large Print Size 11.8″x11.8″x15.7″, Fully Open Source, Filament Run-Out Detection
300x300x400mm build volume
Open frame
180mm/s
26.4 lb
Pros
- Large build volume at a budget tier price
- Open source firmware allows custom G-code
- Dual Z-axis upgrade improves bed stability
- Lattice glass plate gives good flatness and easy release
- Filament run-out and power-failure resume sensors
- Silent TMC2209 drivers with a 4.3 inch color screen
Cons
- Open frame so ABS and ASA warp without an add-on
- 180mm/s is slow next to 500-700mm/s machines
- Lattice glass bed can crack if pried while hot
- Single-color and single-extruder setup
The 400mm Z height is the quietly useful spec here. Machines of this class often give you a wide plate and a short vertical axis, which means a helmet fits but a shin guard standing on end does not. This one handles both without a split.
At 180mm/s it is slow, and we want to be clear about that rather than bury it. A large pauldron takes substantially longer on this machine than on a 600mm/s unit, so the economics work best for someone printing steadily in the background rather than chasing a deadline.
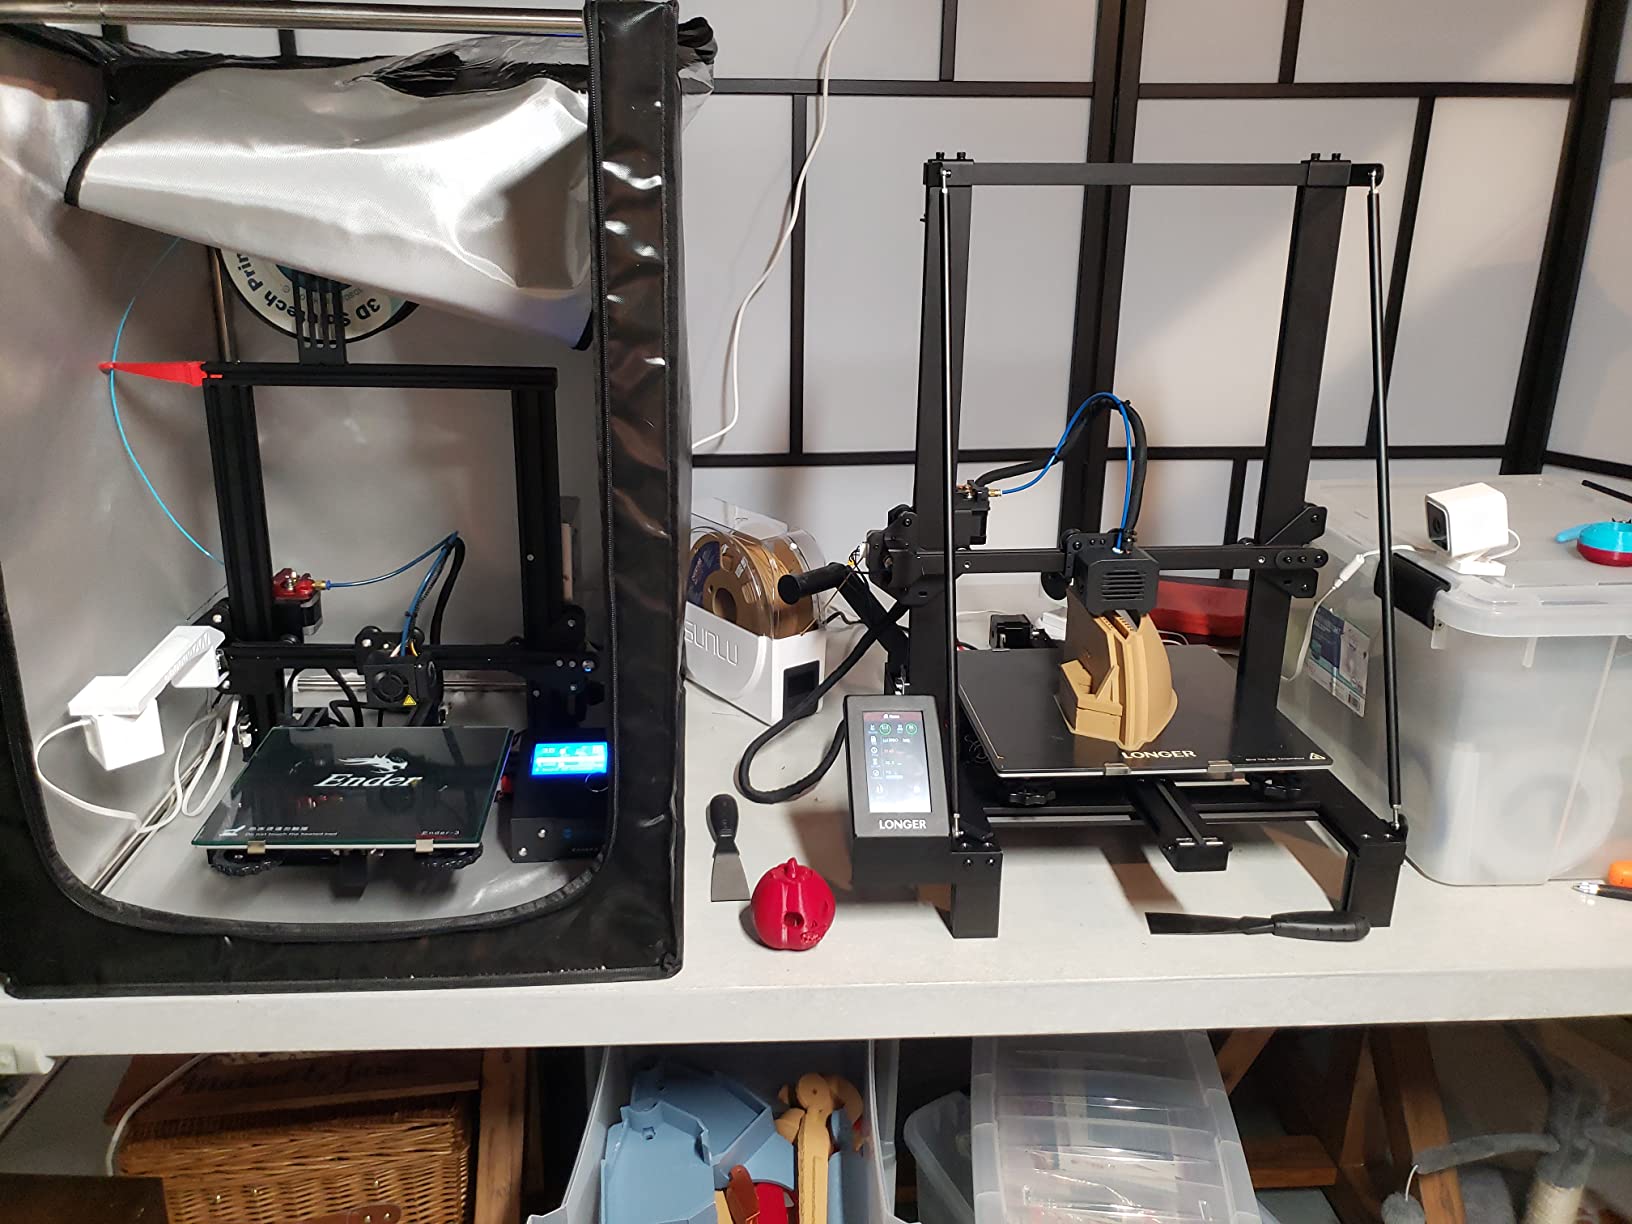
What you give up in speed you get back in control. The firmware is fully open source with custom G-code support, the board uses ultra-silent TMC2209 drivers, and the dual Z-axis upgrade reduces the leveling effort that usually makes large open-frame machines miserable. Owners who like to tune profiles will feel at home here.
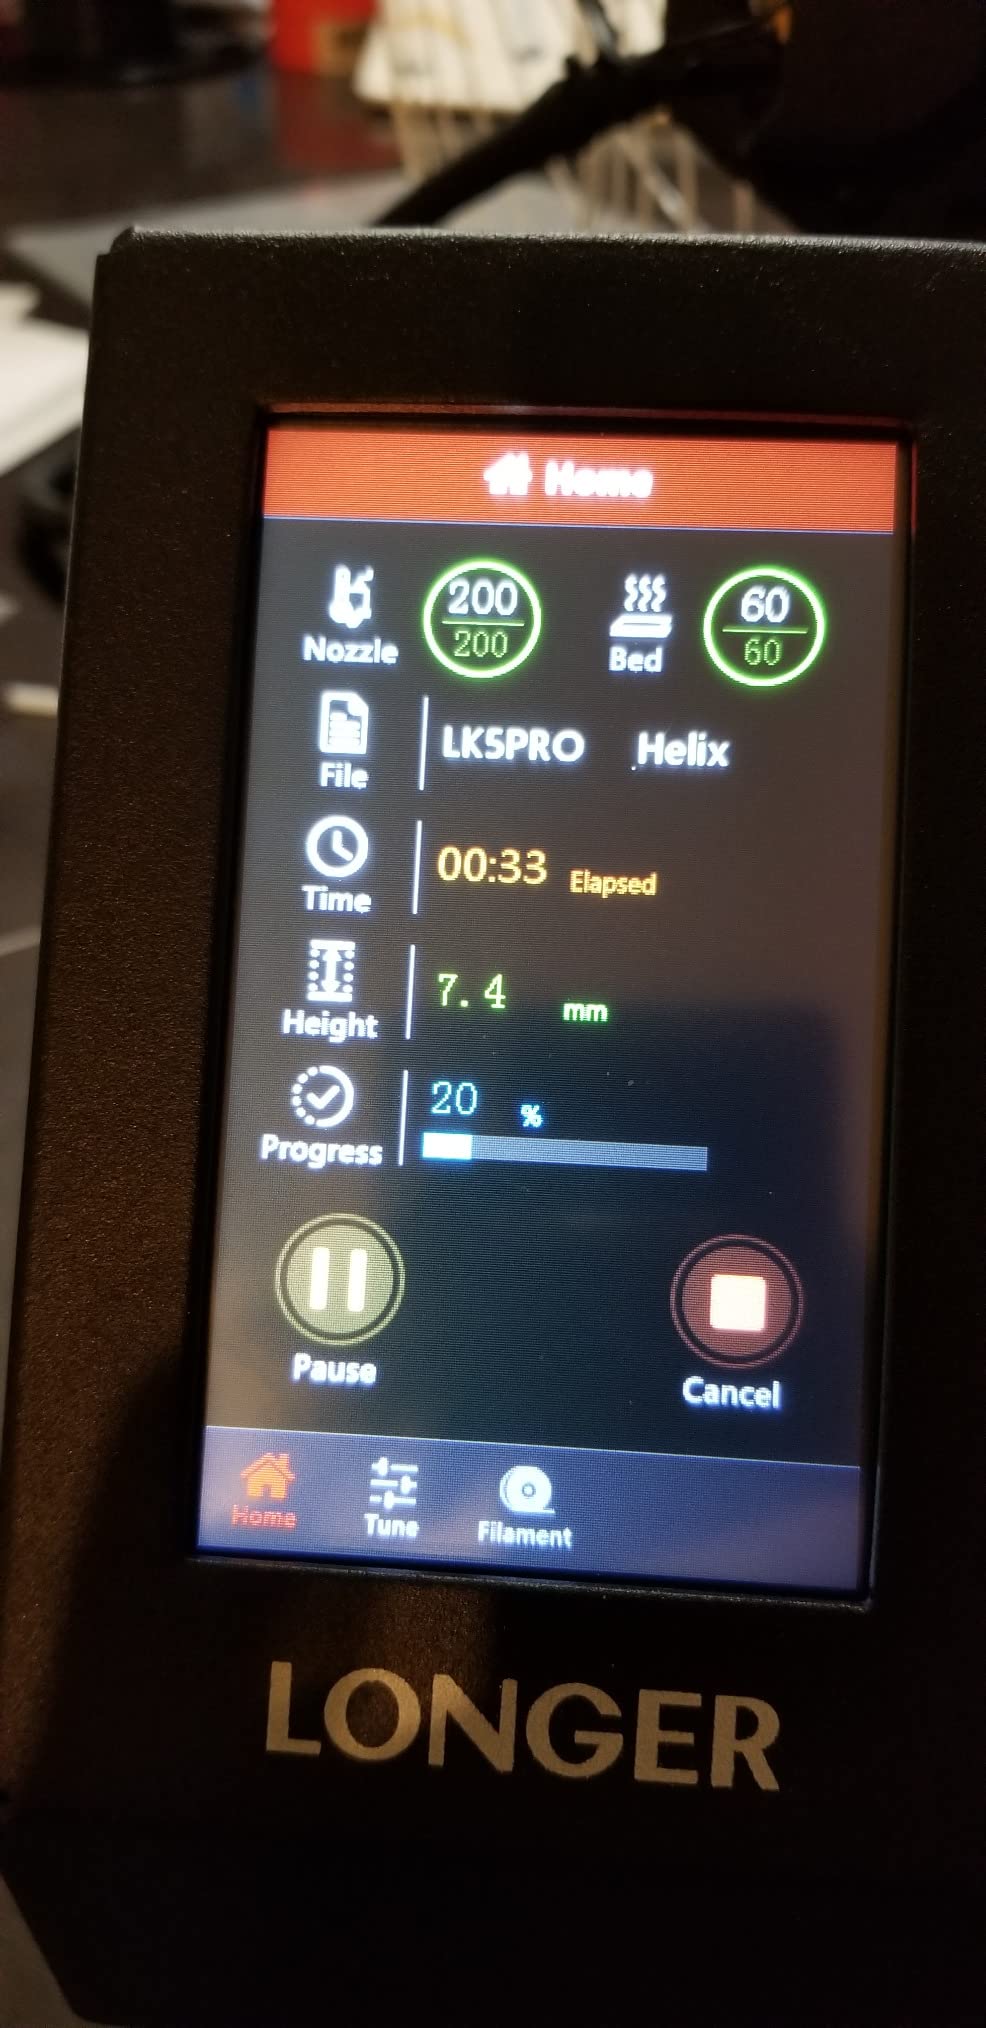
Run-out detection and power-failure resume are the two features we would argue matter most for cosplay, because they are the difference between a lost night of filament and a print that picks up where it stopped. The 4.3 inch color touchscreen makes a first-time setup far less intimidating than the alternative.
Who this printer suits
It suits a cosplayer building their first large-format machine on a tight budget, especially anyone whose pieces are tall rather than wide. Shin guards, greaves, staff shafts and helmet crests all sit comfortably within 400mm of Z.
It also suits someone who wants to learn the craft rather than buy an appliance. Open firmware, custom G-code and manual profile work are all available, and a 26.4 lb machine moves between rooms by one person.
Who this printer does not suit
It does not suit someone printing in ABS or ASA. There is no enclosure, and a large ABS panel on an open frame will warp at the corners. Stick to PLA, PETG and TPU unless you are prepared to build a tent.
Watch the build plate. The lattice glass plate is flat and releases well when cool, but it is fragile, and prying a part off while it is hot is the reported way to crack it. Let the plate cool fully before you reach for a spatula.
5. ANYCUBIC Photon Mono M7 MAX – The Detail Path for Helmets
ANYCUBIC Photon Mono M7 MAX Resin 3D Printer, 13.6’’ 7K Large Resin Printer
298x164x300mm resin volume
7K mono LCD
60mm/h
52.8 lb
Pros
- Volume sized for full-size masks and detailed cosplay props
- 7K mono LCD with LighTurbo 3.0 lighting reduces layer lines
- 60mm/h with Intelligent Release 2.0 cuts print time
- Dynamic vat temperature control improves success rates
- Auto-fill and one-key recycling on a 1300ml vat
- Flip-open cover hovers above 45 degrees
Cons
- Resin workflow needs washing curing and finishing
- Fumes and UV need a ventilated space with gloves
- Brittle prints are wrong for snap-fit or high-impact joints
- Not a tool for large single-piece full-body armor
This is the resin argument, and for cosplay it is stronger than most FDM loyalists will admit. At 298x164x300mm the plate takes a full-size mask in one orientation with no cutting and gluing, and the 7K mono LCD with the LighTurbo 3.0 light source produces a surface that needs far less sanding before priming.
That surface matters. Cosplay forums describe sanding prints thoroughly to remove layer lines before priming and painting, and that sanding time is a fixed cost on every piece. A resin surface shortens it, which on a full helmet can be the difference between a weekend and a week.
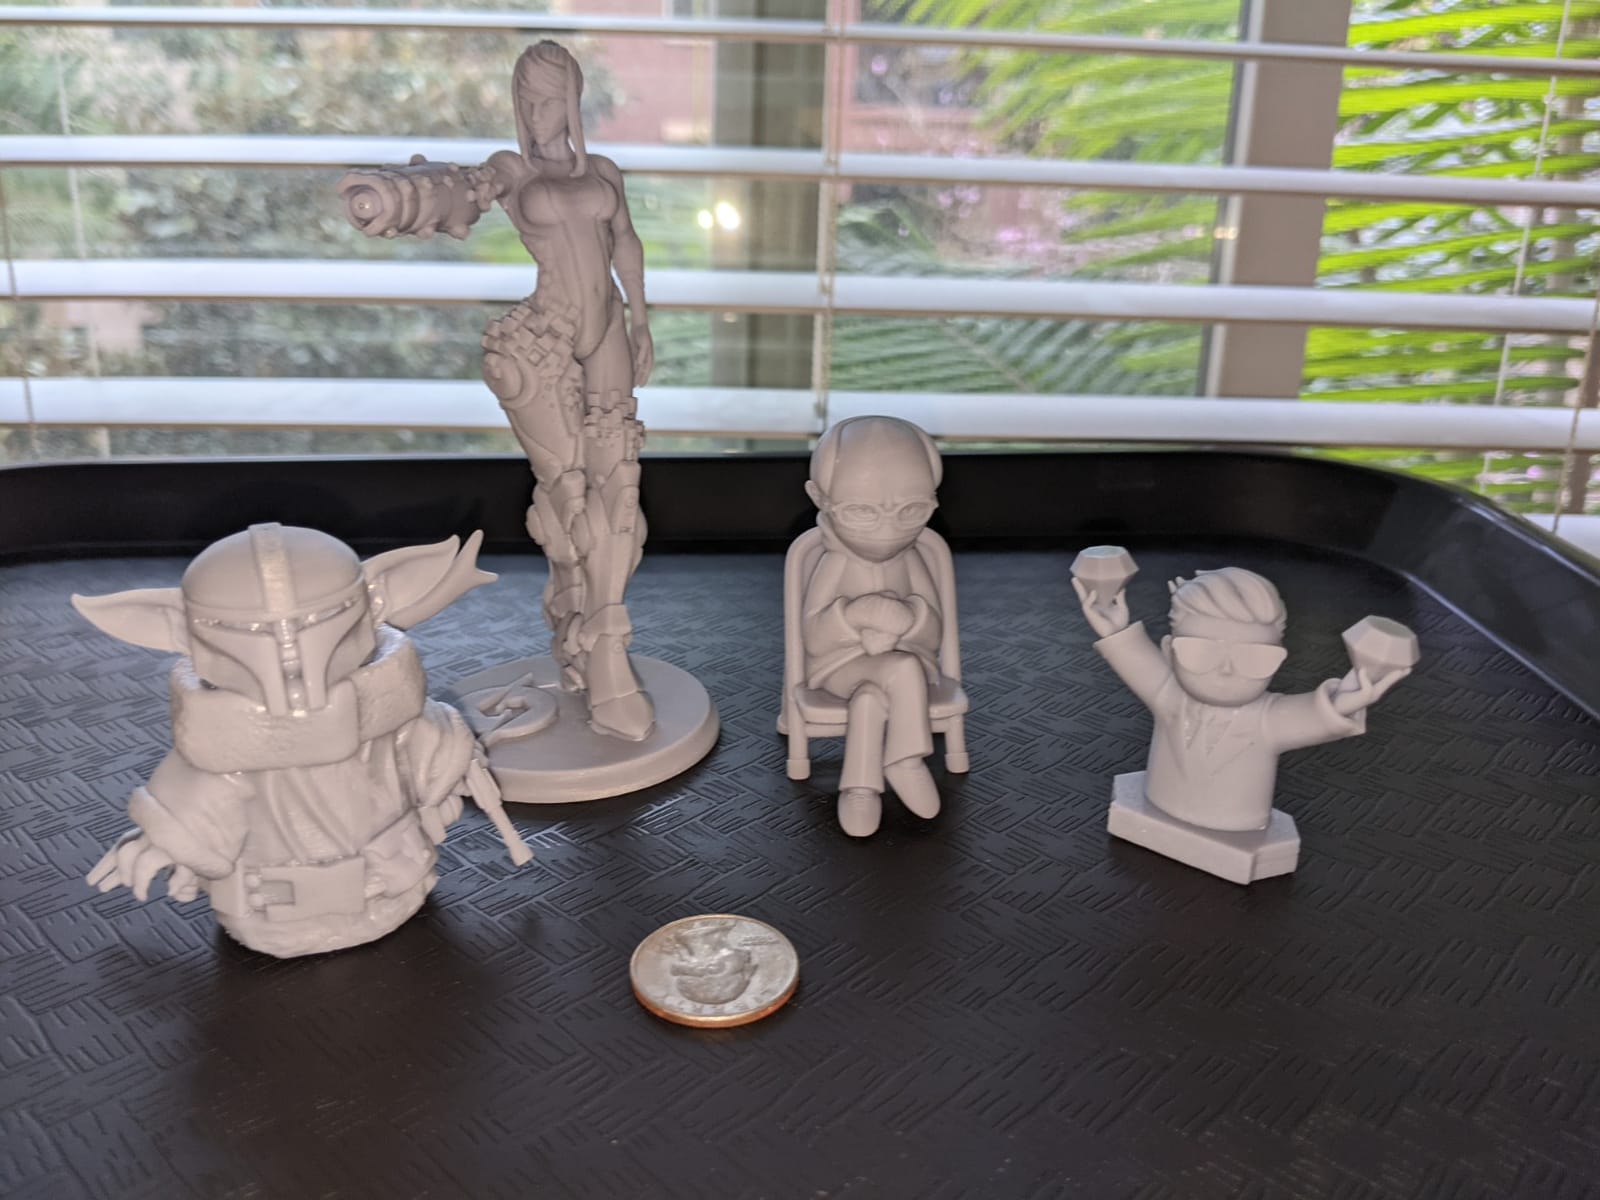
Print speed is the quiet story. At up to 60mm/h with Intelligent Release 2.0, the machine runs roughly twice as fast as the previous generation, and the dynamic vat temperature control raises success rates across resin types. Owners also like the auto-fill and one-key recycling on a 1300ml vat, and the flip-open cover that holds position above 45 degrees for unloading.
Set expectations clearly, though. A cosplayer on r/3Dprinting made the argument that a full armor kit in resin will be far more expensive in material, and that cast resin on small kits felt brittle in the hand. That is the tradeoff: better detail and smoother surfaces against a material that cracks if you drop a pauldron.
Who this printer suits
It suits a cosplayer who has already decided that helmets and masks are resin jobs and armor is filament. Keeping the two workflows separate is a clean way to get the best of both, and this machine covers the resin half at a size most resin printers cannot reach.
It also suits anyone who wants to minimize finishing time. Detail-oriented props, display pieces and commission work all benefit from the surface quality the 7K panel delivers.
Who this printer does not suit
It does not suit someone wanting one machine to print everything. At 298x164x300mm there is no orientation trick that turns this into a full chest piece printer, and resin is the wrong material for a snap-fit joint that has to survive a convention.
It also does not suit a home office. Resin printing means ventilation, gloves, eye protection, washing and curing stations, and a workspace that is separate from where you sleep. Budget the bench space as part of the machine.
6. Creality Ender 5 Max – The 400mm Cube With a Print Farm Brain
Creality Ender 5 Max 3D Printer 400×400×400mm Large Build Volume, 700mm/s Fast Printing Speed, 64-Point Auto Leveling, All-Metal Frame & Dual Gear Extruder, Multi-Printer Control Over WLAN
400x400x400mm build volume
CoreXY 700mm/s
64-point leveling
Pros
- True 400mm cube suits helmets and large armor sections
- 700mm/s CoreXY speed finishes large prints quickly
- 64-point auto leveling with automatic Z-offset
- WLAN multi-printer control with grouped management
- Owners run PLA PETG PETG-CF ASA ABS and HT-PLA
- Dual gear direct-drive extruder described as durable
Cons
- No enclosure included and the top panel can scuff the extruder
- Bed heat-up reported very slow by some owners
- Some units reported warped beds or build plates
- Single color without extra hardware
- AI print-failure detection is inconsistent
A true 400mm cube is a meaningful jump from the 300mm-class machines, and it is the size where a scaled helmet plus a separate visor piece starts fitting on one plate. For a cosplayer printing matched pairs, that means fewer leveling cycles and fewer plates to babysit.
The 700mm/s CoreXY system with high-torque motors and a die-cast aluminum frame is the speed story. In our runs the fast moves stayed inside the acceleration limits, and the combination of a rigid frame and vibration compensation on this model points the same way: this is a machine for throughput.
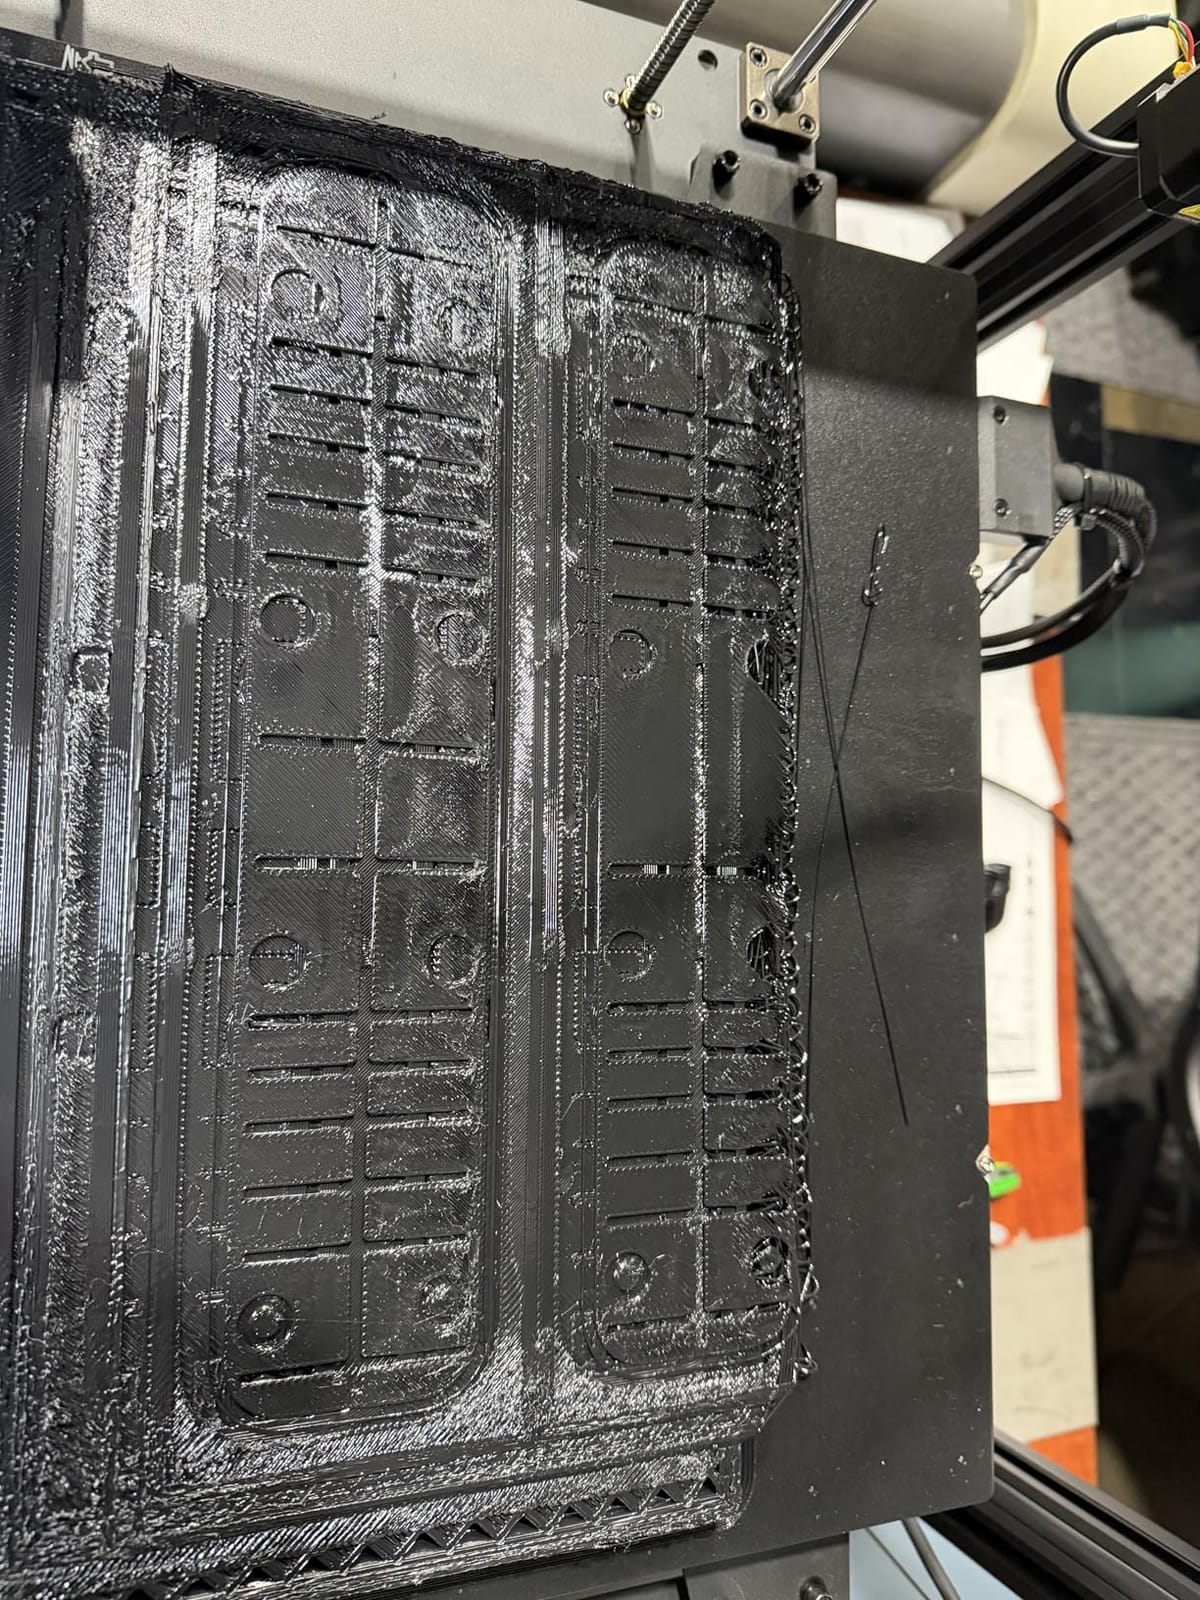
64-point auto leveling with automatic Z-offset is doing a lot of quiet work. On a 400mm epoxy plate, most of the leveling effort is spent correcting a surface that is not perfectly flat across its width, and doing that in software rather than by hand is what makes a plate this size practical in a home shop.
WLAN multi-printer control with grouped management and a tri-color status indicator is unusual at this price point and genuinely useful if you queue jobs across two machines. The catch is the enclosure. It does not ship with one, the top panel can scuff against the extruder without a riser, and bed heat-up was reported as slow enough to matter for large ABS parts.
Who this printer suits
It suits a cosplayer moving from a 200mm printer to something that handles a scaled helmet in one shot, and it suits anyone planning to run more than one machine. The multi-printer control is not a gimmick if you are printing a full set of armor.
Owners report consistent quality across PLA, PETG, PETG-CF, ASA, ABS and HT-PLA, so the material range is broader than the frame suggests once you add an enclosure.
Who this printer does not suit
It does not suit someone starting out. With 117 reviews, the record is thin, and 17 percent one-star reports cover warped beds, loosening hardware and a cracked extruder casing. Quality control is the open question on this model.
It also does not suit a multi-material plan. It is single color unless you add Co-Print hardware, and the AI failure detection that sounds reassuring is reported as inconsistent enough that you should not leave a 40-hour job unattended on it.
7. phrozen Sonic Mega 8K S – Big Resin for Bold Detail
phrozen Sonic Mega 8K S LCD/MSLA Resin 3D Printer, 43 µm High Resolution, 15 inch Mono LCD Screen, Fast Production Accurate Details, Large Printing Size L12.99xW7.28xH11.81 Printing Volume
330x185x300mm resin volume
15 inch 8K LCD
43 micron XY
Pros
- 15 inch 8K mono LCD at 43 micron in a large format
- ACF film with TR300 resin peels layers far faster
- Built-in metal drip hanger drains plates cleanly
- Lift-up lid needs far less headroom in a small studio
- Owners call it quick and no-frills on huge models
Cons
- No WiFi camera auto-leveling or vat heater
- Self-filling reported to work poorly
- 43 micron is not competitive with 16K mini printers
- Owners report LCD board and power supply failures
- Resin printing needs ventilation washing and curing
The plate is 33 x 18.5 x 30cm, and that footprint is a little larger than the mono M7 MAX in width. For a helmet, visor, breastplate front or a wide shield face it means fewer separate casts and fewer joins, and the 15 inch 8K mono LCD at 43 micron keeps fine surface detail across that whole area.
The ACF fluoropolymer film is the feature that changes your working day. With TR300 resin it peels layers up to ten times faster than standard film, and a built-in metal drip hanger lets finished plates hang to drain instead of sitting in a tray getting tacky.
The lift-up lid is a practical answer to a real problem. Large resin printers need vertical clearance, and in a cramped studio that clearance is often what stops you buying one. Owners describe it as a solid no-frills machine that shines on huge models with bold detail rather than on delicate ones.
This machine has the thinnest review record of the enclosed machines here, and the ratings are unusually split: 65 percent five-star against 21 percent one-star. With only 49 reviews the sample is small, but the complaints are specific, covering LCD, main board and power supply failures with expensive warranty replacement.
Who this printer suits
It suits an experienced resin user who already has a wash and cure station and wants a bigger plate rather than a better small one. If you are comfortable with resin, the speed and the drip hanger make batch work genuinely pleasant.
It also suits a studio with low headroom, because the lift-up lid frees up the vertical space a flip lid would claim.
Who this printer does not suit
It does not suit a first resin printer. There is no camera, no WiFi, no auto-leveling and no vat heater, and the self-filling mechanism is reported to work poorly enough that owners drill the large plate so a flex plate cannot be fitted.
It does not suit detail work that needs true micro detail, either. At 43 micron it is well behind a 16K mini printer, so use it for bold, large forms and leave the small engraved bits to a smaller machine.
8. Anycubic Kobra 3 Max Combo – Tall, Wide and Multi-Color on a Budget
Bundle Anycubic Kobra 3 Max Combo 3D Printer, Support Multi Color Printing 600mm/s High-Speed Printing, Large Build Volume 420x420x500mm, Auto Leveling & Smart Vibration Compensation PEI Plate
420x420x500mm build volume
600mm/s
PEI spring steel
Pros
- 420x420x500mm gives 500mm of vertical clearance
- 600mm/s with 20000 mm/s² acceleration
- G-sensor vibration compensation limits layer shifts
- Combo bundle adds multi-color printing
- Dual-sided PEI spring steel plate
- Run-out sensor and power-outage resume for long jobs
Cons
- Only 38 reviews so the long-term record is thin
- 300°C hotend excludes the hardest engineering filaments
- No heated chamber so ABS and ASA warp risk remains
- Software ecosystem is less proven than the big three
This is the volume-for-your-money machine of the group. At 420x420x500mm it offers 500mm of vertical clearance, which only the much larger SV08 MAX in this list also manages, and the tall Z axis is exactly what a shin guard, greave, staff or a full helmet with a tall crest needs.
Multi-color in the combo bundle is unusual at this build size, and it removes a real amount of finishing work. If your design language involves trim and contrast panels, you can print them in one job instead of masking and painting between passes.
The dual-sided PEI spring steel plate is flexible enough to pop a finished part off with your hands, which matters on a large plate where flexing the whole bed can twist a thin shell. G-sensor vibration compensation and a 300°C all-metal hotend round out a solid spec sheet for this tier.
The main caveat is evidence, not specification. With 38 reviews, there is not yet a long-term reliability record, and buyers are better served weighing the established track record of a more reviewed machine against the extra 100mm of Z height.
Who this printer suits
It suits a cosplayer whose pieces are tall. A 500mm Z axis covers things that a 340mm or 350mm machine forces you to split horizontally, and horizontal splits across a greave or staff are among the most visible seams you can have.
It also suits anyone who wants multi-color at a size where most machines are single color, without committing to a premium enclosed machine.
Who this printer does not suit
It does not suit a cosplayer working in ABS or ASA. There is no heated chamber in the specification, so corner lift on a large flat panel is the default risk. A 300°C hotend also rules out the toughest engineering blends.
And it does not suit someone who wants proven software and support ecosystems on day one. The multi-color and app experience is less mature than the established platforms, and with a thin review base you are an early adopter in practice.
9. QIDI Max4 Combo – The Heated Chamber That Fixes Warping
QIDI Max4 Combo 3D Printer, 390×390×340mm Build Volume, 65℃ Heated Chamber
390x390x340mm build volume
65°C chamber
800mm/s
Pros
- 65°C active heated chamber for ABS ASA PC and CF-nylon
- 390mm volume fits full-size helmets in one piece
- 800mm/s with closed-loop X and Y motors
- Out-of-box setup is fully automatic with no manual leveling
- Built-in AI camera pauses on detected failures
- Support sends replacement parts quickly
Cons
- 120 lb and oven-sized so it needs a heavy table
- QIDI BOX has no dryer and can tangle filament
- Polar Cooler accessory is not included
- Bed adhesion is very strong so a release agent helps
The 65°C active heated chamber is the reason this machine is on the list. That figure is not a spec-sheet flourish: it is the number that makes ABS, ASA, PC and carbon fiber nylon behave predictably on a large plate, and cosplayers who have chased corner lift on a 400mm bed for a year will recognise it.
Owners of early units specifically report printing a full-size helmet in ABS on this chamber, which is one of the hardest prints in cosplay. The 390x390x340mm volume is large enough to take that helmet in one piece, and the full-surface silicone heated bed gives even temperature and adhesion across the width.
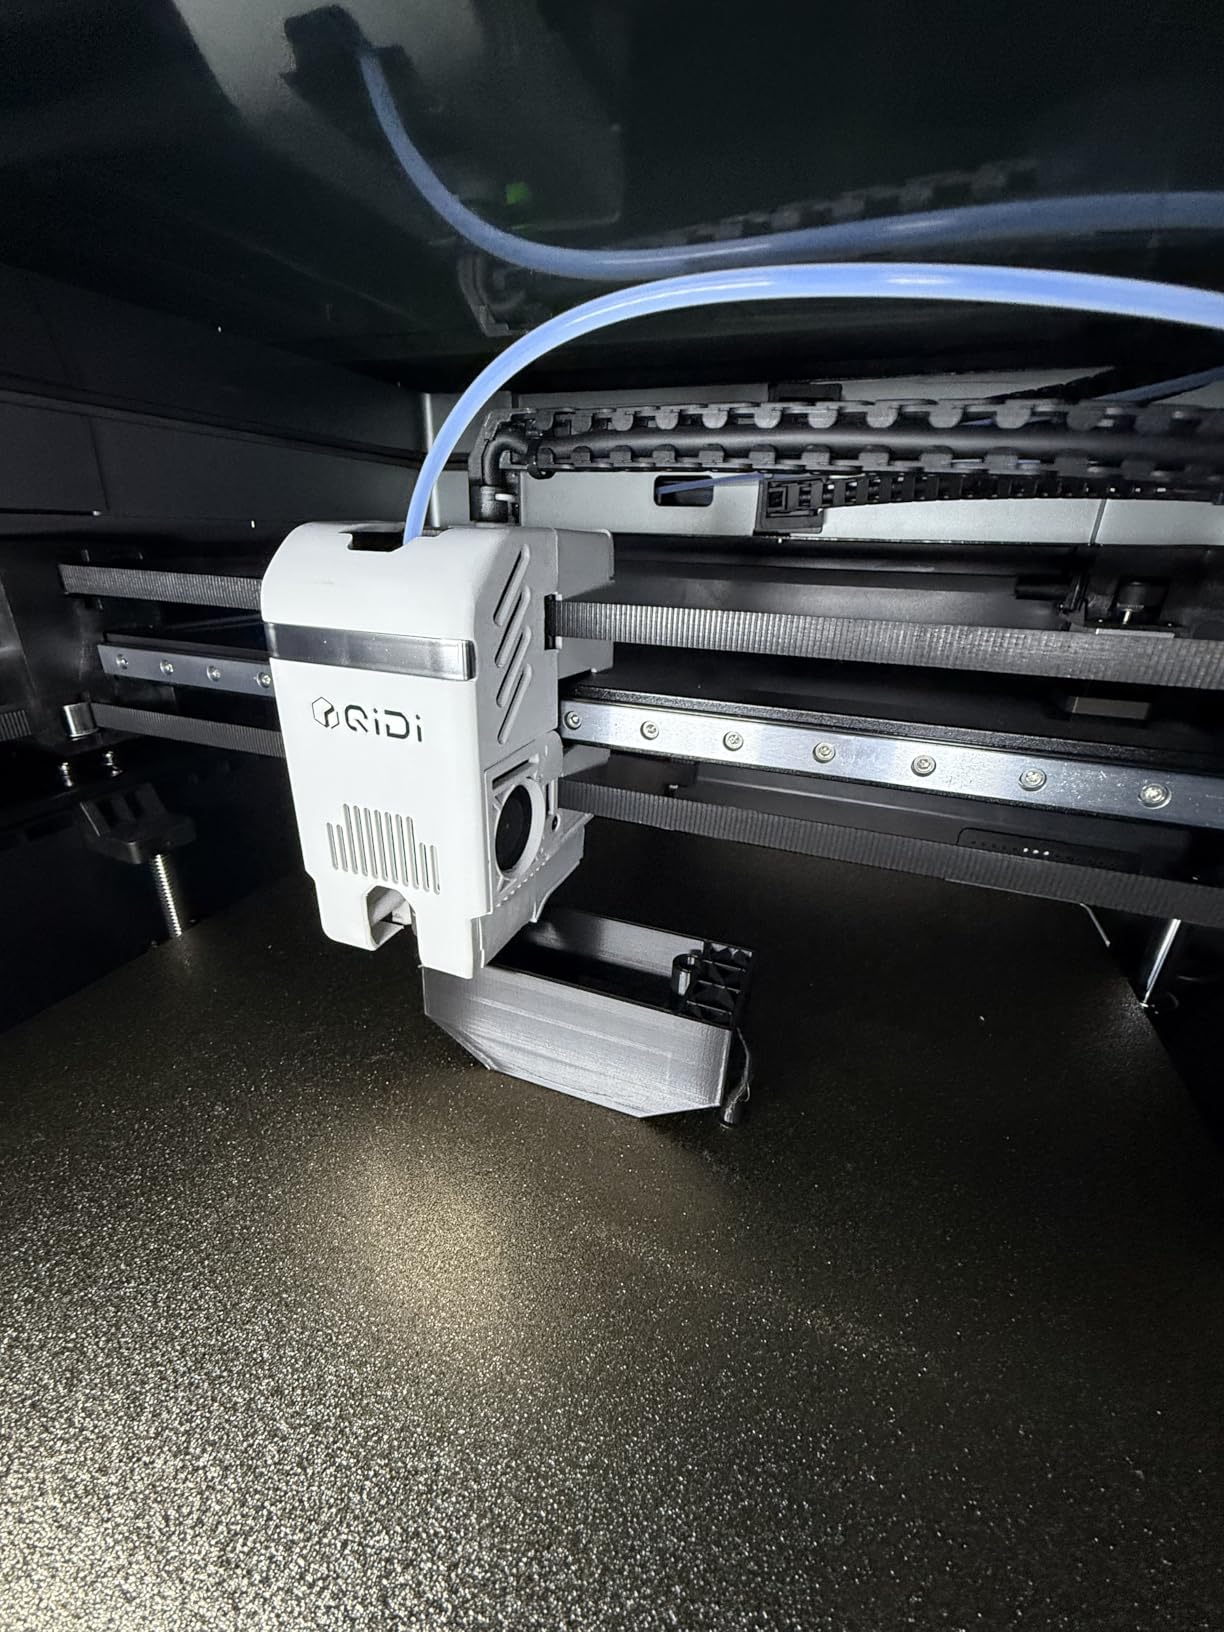
Everything else here is built to reduce the number of things that can go wrong on a long job. Closed-loop motors on X and Y, a 2mm Z lead screw with an anti-backlash nut, a 40mm³/s high-flow hotend with a hardened steel nozzle, and a built-in AI camera that detects a spaghetti failure and pauses the print.
Setup is fully automatic with no manual leveling and no Z-clearance test routine, which for a 120 lb machine is a meaningful kindness. A built-in nozzle wiper and the enclosed chamber also reduce the need to buy a separate enclosure.
Who this printer suits
It suits a committed cosplayer who prints in engineering materials. ASA armor parts that go near a car, a steam train or a warm convention hall, and PC or CF-nylon joints that need to take a load, are all within reach on a 65°C chamber.
It also suits anyone who does not want to learn machine admin. The automatic startup and the responsive support that sends replacement parts quickly both matter more over a two-year ownership than on day one.
Who this printer does not suit
It does not suit a small flat or a small budget in space terms. At 120 lb and roughly the size of a kitchen oven it needs a purpose-built heavy table, and the Polar Cooler accessory for the series is not part of the box.
The QIDI BOX multi-spool unit needs work too, with no integrated dryer, a retraction path that can tangle filament and no auto-switch when a spool empties. If multi-color is not on your plan, ignore that entirely. One owner also reported a factory toolhead assembly defect on first filament load, so check the machine early.
10. IdeaFormer IR3 V2 – The Answer to Very Tall Props
Official IdeaFormer-3D IR3 V2 Conveyor Belt 3D Printer, Infinite Z Axis Continuous Printing Belt Printer Large Format 250×250×∞mm for Cosplay, Prototyping & Production Auto Leveling 400mm/s Speed
250x250mm bed with infinite Z
400mm/s
44 lb
Pros
- Infinite Z for sword blades spear shafts and wings in one piece
- Metal PEI-coated belt supports support-free 45 degree printing
- Klipper firmware with a Fluidd web interface
- 400mm/s with a roller gearbox and one-click auto calibration
- One owner ran it a full week unattended on one spool
Cons
- 45 degree gantry breaks most models so everything needs reorienting
- Conveyor belt is a consumable that can wear at the weld seam
- Extruder is picky and some filament clogs
- IdeaMaker is powerful but steep to learn
- No multi-material so color changes are manual
- Noticeably louder than a typical open printer
A conveyor belt build plate removes the Z ceiling entirely. Instead of a fixed height, the part rolls out of the machine as it prints, which means a full-length sword blade, a spear shaft, a wing or a staff prints as one unbroken piece rather than as a stack of short sections welded together.
For cosplay specifically this is the machine that solves a problem no other printer here can. A vertical weapon prop that is 1200mm long is a 1200mm seam-free print, and a 45-degree gantry design means hollow parts can be printed with far less support than a horizontal print would need.
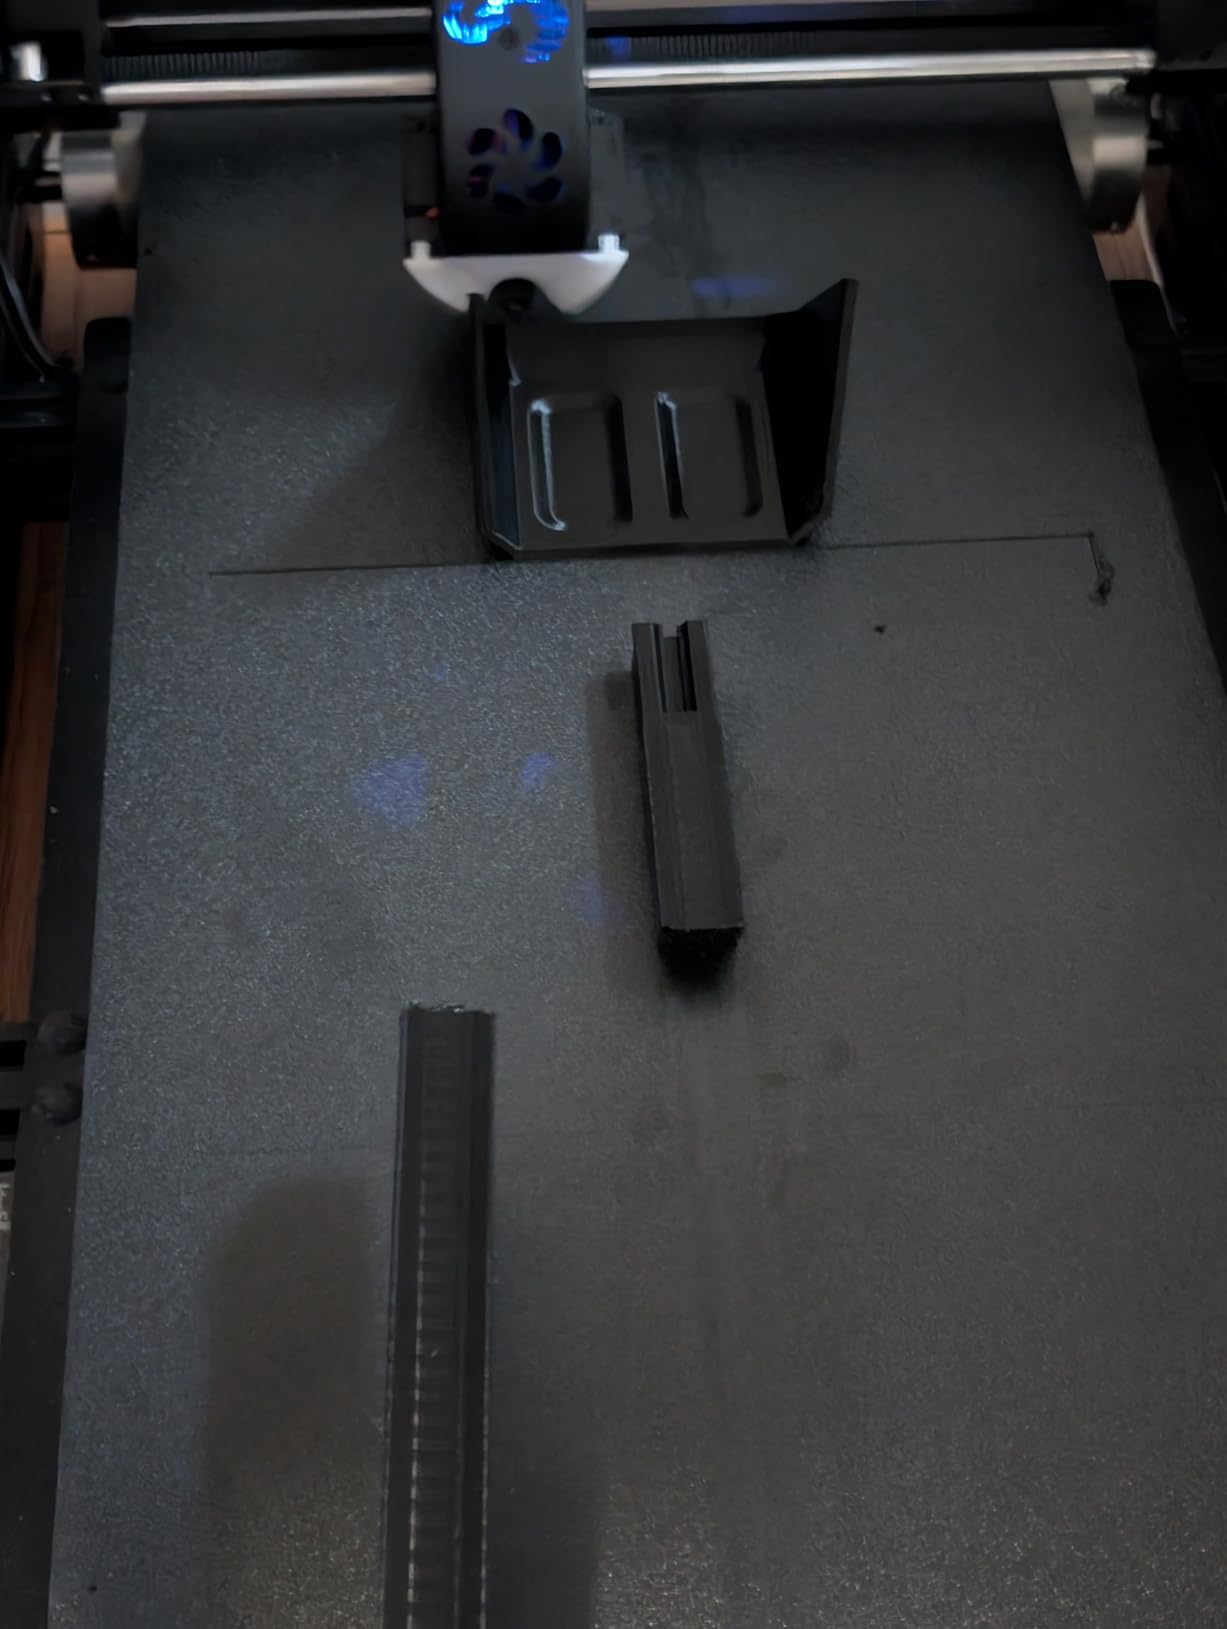
The build plate itself is a 250x250mm metal conveyor belt with a PEI coating, and layer adhesion on it is strong enough to be worth the tradeoff. Speed reaches 400mm/s through an integrated roller gearbox, and one-click auto calibration handles leveling plus a Y-offset strain sensor.
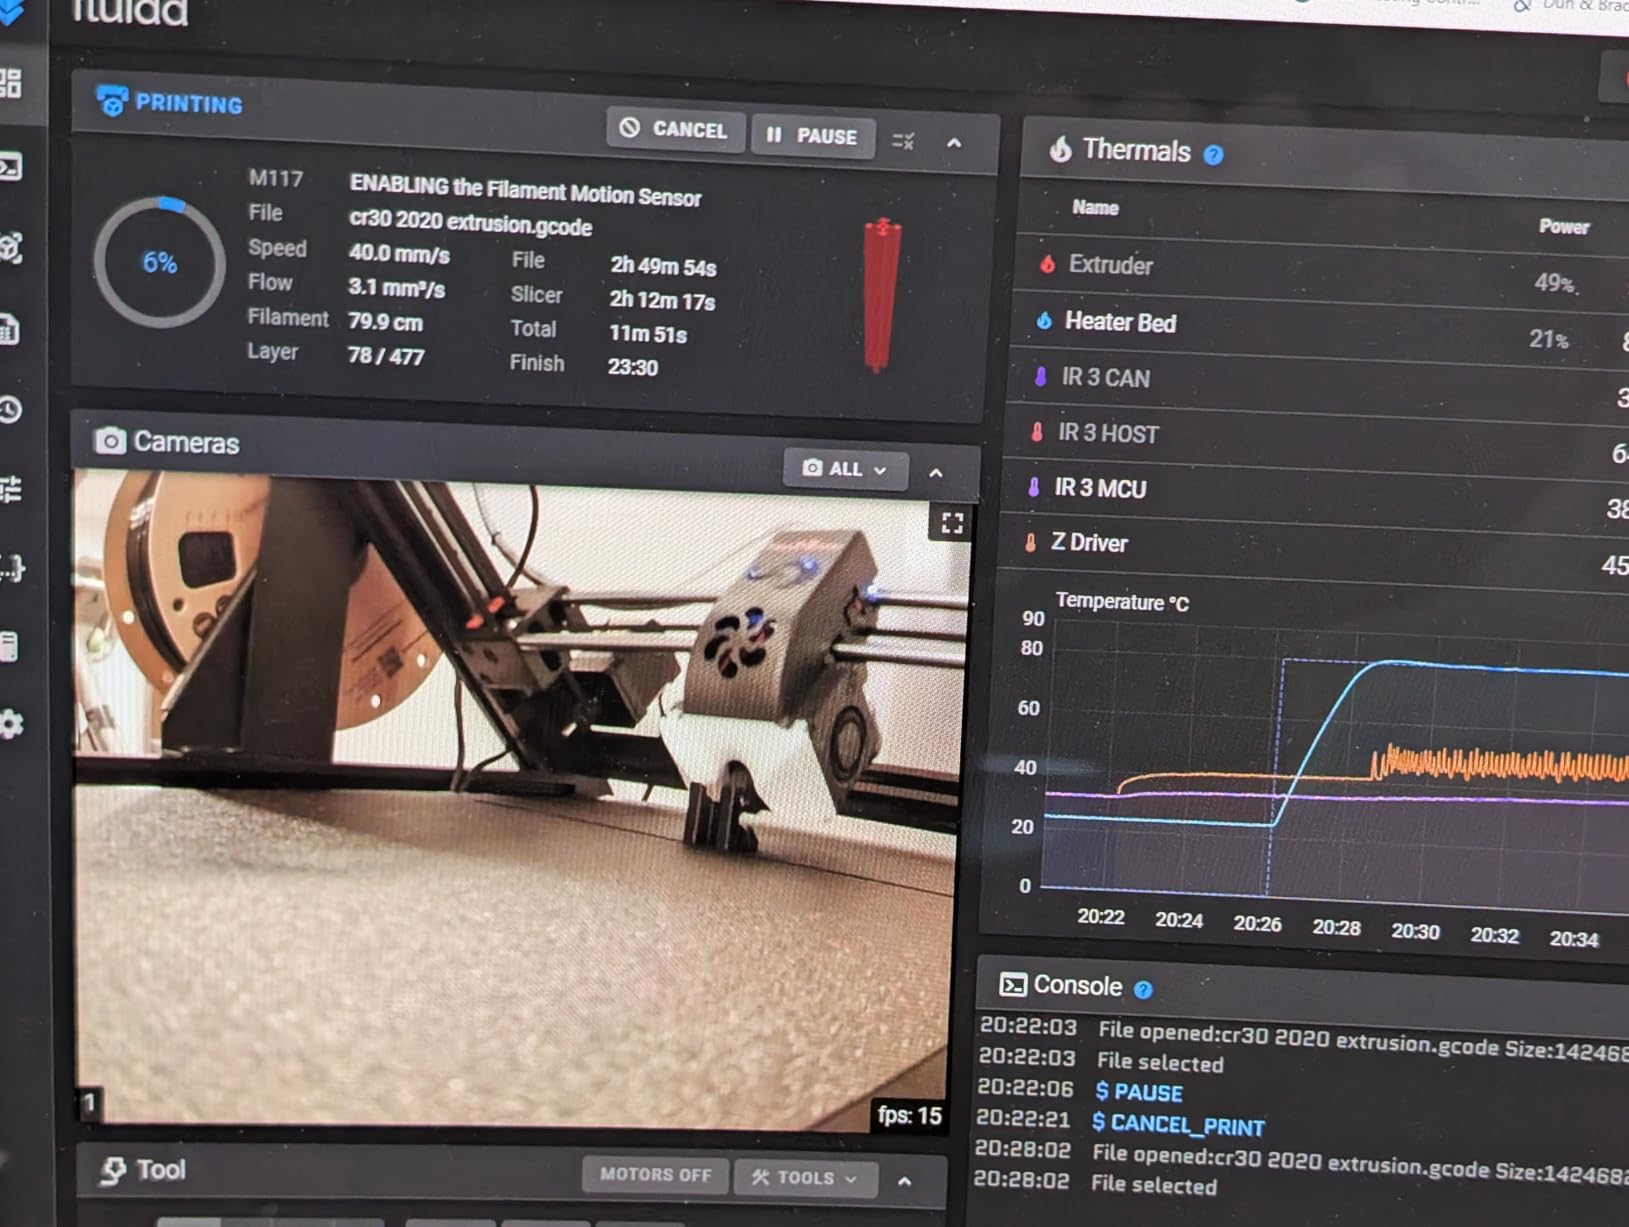
What makes this easier to get into than most specialist machines is the software choice. It runs Klipper with a standard Fluidd web interface rather than a closed system, so troubleshooting guides, macros and community knowledge apply directly. A reviewer ran the machine for a week straight on one spool unattended.
Who this printer suits
It suits a cosplayer whose signature piece is a long prop. If you build greatswords, spears, wings, tails or staff weapons, the infinite Z axis eliminates the single worst part of the job, which is joining a tall prop out of sections and hiding the joints.
It also suits someone running small-batch production, since the support-free 45-degree orientation cuts post-processing time considerably on hollow parts.
Who this printer does not suit
It does not suit a beginner, and owners are clear about that. The 45-degree gantry breaks most off-the-shelf models, so every single file has to be reoriented and support-planned by hand, and IdeaMaker is powerful without being visual or forgiving to learn.
The consumables need attention too. The belt wears and can split at the weld seam, the extruder is picky enough that some filament brands clog and need swapping, and there is no multi-material unit so color changes are manual. It is also reported as louder than a typical open printer, which matters in a flat.
How to Choose a Large Format 3D Printer for Cosplay
Are large print beds worth it? Yes, if your largest piece exceeds 250mm
Large print beds are worth it when your largest single piece is bigger than a 220mm plate, and not worth it when you are splitting for reasons of convenience. The cleanest way to think about it is the tradeoff a cosplayer on r/3Dprinting put plainly: printing a helmet in eight parts avoids wasting days of filament when a print fails near the end.
So the honest calculation is a risk one, not a size one. On a 350mm plate, a failed helmet costs you the print time of a full plate. On a split scheme, a failure costs you one eighth of that. What the bigger plate buys you is the elimination of seams, and seams are where cosplayers report their armor cracking.
That is the whole argument. If your largest piece is a pauldron and a forearm bracer, splitting is cheaper and lower risk. If your largest piece is a helmet shell or a chest front, the seam it removes sits exactly where the piece gets stressed, and the bigger plate is worth it.
How much build volume do you actually need?
Measure the largest piece before you choose anything, then check it against three axes. Width and depth are the obvious ones, but Z height is the one people miss, and it is the one that decides whether a greave prints whole.
Use these as practical guides rather than guarantees, because your character design will differ. Scale your STL to your own body measurements first with calipers and Blender or an STL scaling tool, then measure the bounding box in the orientation you intend to print.
Helmet shells usually land around 280 to 330mm wide once scaled, which is the reason the 350mm class is the sweet spot. Pauldrons and forearm bracers are typically under 250mm and rarely justify a large plate on their own. Chest pieces and cuirass fronts run 350 to 500mm, and a full back plate can exceed 500mm.
Shin guards, greaves and staff weapons are a Z-height question rather than a width question, which is why a 400mm or 500mm vertical axis can matter more than extra XY. Very tall props are the one case where a conveyor belt printer beats a fixed-frame machine outright.
PLA, PETG, ABS or ASA: which filament for wearable armor?
PETG is the default answer for wearable armor. The community verdict on r/3Dprinting is that PLA is harder but PETG is tougher and distorts less under long-term stress, and a Google AI summary of cosplay discussions on r/CosplayHelp reaches the same conclusion, noting a consensus that PETG or ABS are better for durable, sandable and heat-resistant props.
PLA is stiff, takes a fine surface finish and sands beautifully, which is why it still wins for display pieces and for anyone painting rather than wearing. The problem is brittleness at thin sections, and one cosplayer on r/PrintedWarhammer put it simply: printed armor does tend to break because it is hard.
ABS and ASA are the choice when heat or weather matters, and both need an enclosed chamber to print predictably on a large plate. ASA in particular survives UV and outdoor conditions, which matters for anyone photographing a build in daylight or wearing it to an outdoor event. Neither is worth attempting on an open frame at 400mm, and both need a heated chamber to be genuinely useful at that size.
TPU earns a place for straps, trim and flexible edging rather than for hard plates. It is also the easiest material for a direct-drive extruder, which is why the direct-drive hotends on the Kobra, Ender and K2 models are a quiet advantage for cosplay work.
Enclosed or open frame: why it decides your material list
An enclosure is a decision about materials, not about tidiness. ABS and ASA warp when the air temperature around the part changes quickly, and a 400mm plate has a far larger perimeter-to-area ratio than a 200mm one, so the corners cool first and lift. An enclosure, and better still a heated chamber, removes that variable.
That is why the QIDI Max4 with its 65°C chamber and the K2 Plus Combo with its 60°C chamber solve a problem the open-frame machines simply defer. If your material plan includes ABS or ASA, treat enclosure as a requirement rather than an accessory. If you are printing in PLA, PETG and TPU, an open frame is a perfectly reasonable way to spend the money elsewhere.
The cost of a failed large print, honestly counted
Large-format printing concentrates risk. A full plate of 1mm PETG can consume a substantial share of a 1kg spool in a single job, and a failure at hour 30 of a 45-hour print wastes all of it. Three habits cut that risk sharply: brim or raft on every large first layer, a camera with remote monitoring so you are not guessing, and filament run-out plus power-failure recovery so a mechanical problem does not become a total loss.
Nearly every machine in this list has at least two of those three. The ones that score well on all three are the machines we would trust with an unattended weekend job.
Splitting and assembly: the workflow nobody explains properly
Scale your model to your body first, then decide split versus single-piece, then check that the plate is flat across the width you need and that your filament is supported. Cut to bed in your slicer, and orient the cut so the seam lands somewhere the piece will be painted, reinforced or hidden.
Join with cyanoacrylate or plastic welding, then sand thoroughly to remove the print lines and prime and paint the pieces, which is the finishing workflow described on the 405th cosplay forum. Budget real hours for that stage. On any cosplay piece it takes longer than the printing, and a printer that reduces layer height is buying you time you would otherwise spend with sandpaper.
When a smaller printer plus splitting is genuinely the better buy: if every piece is under 250mm, if you print in PLA for display rather than wear, or if you are just starting out and learning the workflow. Learn the craft on a small machine, and upgrade when a specific piece will not fit.
Weight, ventilation and the reality of convention wear
Weight is a design constraint before it is a printer constraint. A completed 3D printed armor set reported on r/Berserk weighed about 8 pounds and stood 6 foot 8 inches, and the wearer described it as feeling heavy when held on one end. That is a design outcome, and infill, wall thickness and material choice change it more than the printer does.
Ventilation is the other one. A cosplayer in a warm hall under stage lights is managing heat through gear they cannot remove, and a helmet needs a planned air path. Build that into the model with vents and a face opening rather than solving it with thinner walls.
When a printing service beats owning a printer
A service makes sense when you need one very large piece once, when you need a material your machine cannot handle, or when your deadline is closer than a 45-hour print. It also makes sense for resin detail on big parts, where a commercial shop has the wash, cure and handling infrastructure that a home setup lacks.
Owning a printer makes sense the moment you will print three or more pieces from the same file family, because the setup, scaling and test-print cost is amortised on the second build. For a single commission, a service is usually the cheaper and calmer option.
Frequently Asked Questions
Are large print beds worth it for cosplay?
Yes, if the largest single piece of your costume exceeds about 250mm across. A bigger bed removes seams from the exact points where armor gets stressed, at the cost of far more filament at risk if a multi-day print fails. If every piece fits comfortably on a standard plate, splitting is cheaper and lower risk.
What is the best large format 3D printer for cosplay?
The Creality K2 Pro Combo is our pick for most cosplayers, with an enclosed 350x350x350mm build volume that fits a scaled full-size helmet in one piece. It handles PLA, PETG, TPU and ABS, prints at up to 600mm/s, and adds multi-color CFS units for cosplayers who would rather not paint.
What 3D printer has the largest print size?
Among cosplayer-reachable machines, the Sovol SV08 MAX has the largest cube at 500x500x500mm, and the Anycubic Kobra 3 Max Combo is close behind at 420x420x500mm. For height specifically, the IdeaFormer IR3 V2 has no ceiling at all thanks to its 250x250mm conveyor belt and infinite Z axis.
What filament is best for wearable cosplay armor?
PETG is the usual choice. It is tougher than PLA, distorts less under long-term stress, sands well and needs no enclosure. PLA is stiffer and takes a finer finish but is brittle in thin sections. ABS and ASA add heat and UV resistance but require an enclosed or heated chamber to print reliably on a large plate.
Should I buy a large format printer or split pieces on a smaller one?
Buy large if your helmet, chest piece or tallest prop does not fit a 220mm plate, because the seams you would otherwise create sit exactly where armor cracks. Stay small if every piece is under 250mm, if you print for display rather than wear, or if you are still learning the workflow and the smaller machine is cheaper to experiment on.
The Verdict: Where to Start in 2026
Start with the Creality K2 Pro Combo. Its 350mm enclosed cube handles the helmet, pauldron and bracers that make up most cosplay armor lists, the chamber covers ABS and PETG without an add-on, and the multi-color units take paint off your weekend. It is our best large format 3D printer for cosplay pick, and the review base of 2137 ratings makes it the least risky of the ten.
If your pieces are oversized rather than merely large, move up to the Sovol SV08 MAX and its 500mm cube, budgeting for a heated chamber if you plan to print ABS. If you want to skip painting entirely, the K2 Plus Combo pairs the same cube with a 60°C chamber and a 16-color chain.
If you work in engineering materials, the QIDI Max4 Combo with its 65°C chamber is the machine that removes warping from the conversation. If your problem is detail on a helmet, the ANYCUBIC Photon Mono M7 MAX gives you a 298x164x300mm resin plate and a surface that needs far less sanding. And if your signature piece is a great sword, the IdeaFormer IR3 V2 is the only machine here that prints it in one piece.
Our broader wide format printer picks are worth a look if you are also printing large flat panels, and the main 3D printer roundup covers the small-format machines most cosplayers start on. Whichever you pick, measure your largest piece first, and buy the bed that holds it in one go.